Bell Furnace Factory Best Practices for Quality Heat Treatment
2026-10-16
Quality heat treatment in a bell furnace factory isn’t achieved by luck; it’s engineered through exacting best practices that are easy to overlook until a load comes out wrong. At THINKING-LONG, we’ve built our reputation on those unglamorous details. Here’s what actually works on the floor—and why it matters for every batch you run.
Getting Temperature Uniformity Right Without Overcomplicating It
Achieving even heat distribution rarely calls for exotic hardware or endless tuning. Most real-world uniformity problems trace back to a handful of overlooked details: sensor placement too close to heating elements, airflow paths that create dead zones, or insulation gaps that silently bleed heat. Fix those first, and the temperature spread often tightens on its own.
Consider the load itself before adding more control loops. A densely packed chamber behaves differently than an empty one, and the same settings won't suit both. Instead of chasing a perfect setpoint, map the actual gradient under your typical operating conditions. Then adjust baffles, fan speed, or rack spacing to disrupt the natural hotspots—small mechanical changes frequently outperform software tweaks.
Finally, resist the urge to over-instrument. A few well-placed thermocouples that you actually trust tell you more than a dozen noisy sensors feeding a dashboard. Calibrate against a reference periodically, document what works for your specific setup, and let the process settle. Uniformity is a habit of design and maintenance, not a number to force.
Atmosphere Control Choices That Prevent Surface Oxidation
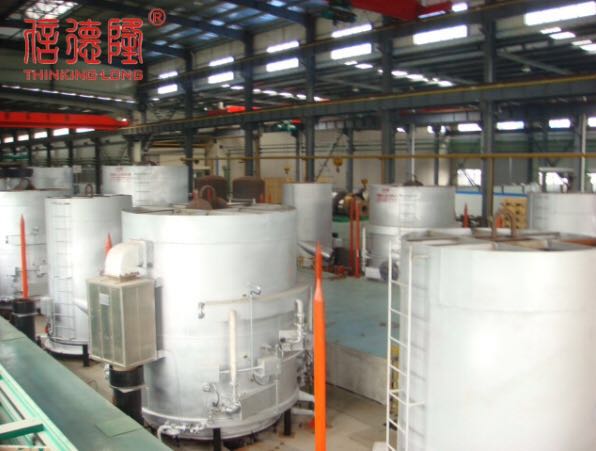
Choosing the right protective atmosphere during thermal processing is often what separates a bright, clean metal surface from one marred by oxide scale. The most direct approach involves flooding the furnace with an inert gas such as argon or nitrogen, which physically displaces oxygen before it can react. For many non-ferrous metals and certain steels, pure nitrogen works well, but its effectiveness drops sharply if trace moisture or leaks persist. A more aggressive option is using a reducing atmosphere, typically a blend of hydrogen and nitrogen. Hydrogen actively scavenges any residual oxygen by forming water vapor, which is then carried away. This approach is particularly favored for stainless steels and copper alloys where even a faint oxide tint is unacceptable. The exact ratio depends on the alloy and temperature, with higher hydrogen levels needed for chromium-bearing materials.
Vacuum furnaces offer another powerful route to prevent surface oxidation, especially when processing reactive metals like titanium or zirconium. By lowering the chamber pressure to levels where oxygen is negligible, oxidation is suppressed without introducing any reactive gases. The trade-off is cycle time and equipment cost, since heating in a vacuum relies on radiation rather than convection. Still, for parts requiring the absolute cleanest surface—such as medical implants or aerospace components—the vacuum approach remains unmatched. Some shops combine both strategies: a rough vacuum to pull out air, followed by backfilling with an inert gas to improve heat transfer while maintaining a non-oxidizing environment. The choice ultimately hinges on the material's sensitivity, the required surface quality, and the production budget.
Practical details often determine whether an atmosphere control strategy truly prevents oxidation. Furnace door seals must be tight, gas purity needs to be verified at the point of use, and the workload should be thoroughly dried before entering the hot zone. Even small amounts of lubricant residue or moisture on the parts can consume the protective atmosphere locally and create spot oxidation. Flow rates also matter: too low allows air ingress, while too high wastes gas and can disturb temperature uniformity. For batch operations, purging cycles should be validated by measuring oxygen levels at the exhaust, not just by timer. Ultimately, the most reliable oxidation prevention comes from matching the atmosphere composition to the specific alloy, monitoring the environment continuously, and keeping human handling to a minimum before and after the process.
Smart Loading Patterns for Even Heat Distribution
Achieving even heat distribution isn't just about how much you load—it's about how you arrange it. Instead of clustering dense items in the center, leave intentional gaps that let hot air circulate freely. A ring-shaped arrangement around the edge, with the tallest item slightly off-center, often works better than a packed grid because it prevents cold pockets from forming near the walls.
For mixed loads, place slower-cooking or denser pieces toward the outer zones where heat tends to peak, while quicker-cooking items can sit closer to the middle. Rotating the container halfway through the cycle also compensates for natural hotspots, but the real trick is to avoid stacking flat layers that trap steam. A slightly uneven, mindful layout usually beats a perfectly symmetric one when you're chasing uniform doneness.
Maintenance Habits That Keep Bell Furnaces Running Smoothly
Most bell furnace issues start small: a hairline crack in the inner bell refractory, a slightly lazy flame scanner, a seal that is not seating evenly. Checking these right after a cycle ends—while the shell is still warm—reveals stress patterns that disappear once everything cools. Record the location and length of any spalling instead of just noting 'minor damage' in the log.
Burner maintenance goes beyond cleaning tips. The UV sensors and flame rods collect an invisible film after a few reducing-atmosphere runs, which shifts their threshold and leads to nuisance trips or delayed ignition. Wipe them with a dry lint-free cloth and verify the sight tube alignment every three to five cycles. Drain the gas train condensate traps at the same interval, especially in humid months.
Seal and atmosphere control matter more than many people think. If the sand or ceramic fiber seal at the base is uneven, it creates a pressure leak that distorts the protective atmosphere and can oxidize the load near the rim. Keep the seal depth consistent rather than adding extra material 'just in case.' Listen to the circulation fan on startup—bearing wear often shows up as a low-frequency rumble before it becomes visible vibration.
Training Operators to Spot Heat Treatment Issues Early
Most heat treatment failures don't announce themselves with a bang. They start quietly: a slight color shift on a batch of gears, a furnace thermocouple reading that wavers just outside the usual band, or a quench tank that takes a few seconds longer to recover temperature. The trick is teaching operators to notice these small deviations before they turn into scrap or, worse, a field failure. That means building familiarity with what 'normal' actually looks like for each furnace and each part family—and making sure the floor crew trusts their own observations enough to speak up.
Short, focused training sessions work better than day-long slide decks. Walk operators through real examples of early warning signs using photos and actual parts that were caught in time. Pair newer staff with someone who has seen years of quirks in the same equipment. And keep a simple one-page checklist near each station, not a 40-page manual, so the knowledge stays usable when things get busy. The goal isn't to turn operators into metallurgists; it's to sharpen their attention so problems get flagged while there's still room to adjust.
Final Inspection Steps That Verify Consistent Quality
Before any batch leaves the floor, each unit goes through a hands-on check that mirrors how a customer would actually use it. We pull samples at random rather than only looking at the first few off the line, because defects often show up in the middle of a run. The inspector checks alignment, surface finish, and any moving parts under normal load, not just in a static position. If something feels slightly off—even if it still passes the written spec—it gets set aside for a second look.
After the physical review, we cross-reference the measured values against the approved golden sample and the previous three batches. This catches slow drift in tooling or material batches before it becomes a field failure. Each inspection record is signed with the time and the specific gauge used, so if a question comes up later, we can trace exactly which shift and which instrument produced the reading.
FAQ
Temperature uniformity, soaking time, atmosphere dew point or carbon potential, and cooling rate are the ones that usually make or break a cycle. We calibrate thermocouples regularly and use multi-point load thermocouples on every new product setup to verify the actual temperature spread before signing off on the recipe.
Balancing the heating zones and adjusting the circulating fan speed inside the retort helps a lot. It is also worth checking that parts are not packed so tightly that they block the gas flow. Running periodic empty and loaded temperature profiling studies will show you exactly where the cold and hot spots are.
Keep a close eye on seal condition, retort distortion, and burner or element performance. Carbon buildup on the inner cover can change heat transfer, so cleaning schedules matter. Calibration of temperature and atmosphere instruments should be on a fixed calendar, not just when something looks off.
Without a controlled atmosphere you get oxidation and decarburization, especially on bright annealing work. The ratio of nitrogen to hydrogen and the dew point need to be held within a narrow band, otherwise surface finish and carbon content start moving away from specification.
Leave clear flow paths for the circulating atmosphere and keep consistent spacing between parts. Put heavier or thicker sections toward the center and lower part of the load where heating is slower. Avoid dense stacking in one area because that creates a different cooling rate than the rest of the load.
Soaking time starts only after the coldest part of the load reaches target temperature, not when the furnace control thermocouple does. Use load thermocouples placed in the slowest heating location and base the soak on the largest cross-section in that load. This prevents both under-soaking and unnecessary oversoaking.
Surface oxidation, uneven hardness, distortion, and case depth variation are common. Prevention usually comes down to tighter atmosphere control, better load arrangement, slower ramp rates for distortion-prone parts, and checking that the cooling phase does not create too much thermal gradient.
Operators need to understand the thermal cycle curves, not just press start. They should be able to spot an abnormal trend early and know when to hold a load for inspection. Standard operating procedures with clear pass/fail limits and periodic refresher training keep everyone from drifting back into bad habits.
Conclusion
Achieving dependable heat treatment in a bell furnace starts with a practical approach to temperature uniformity—no need for exotic control schemes when careful thermocouple placement and periodic profiling already expose cold spots. Pair that with atmosphere selection matched to the workload: for most carbon and low-alloy steels, a simple nitrogen-methanol blend or endothermic gas keeps decarburization and scale at bay without the cost of vacuum purging. Loading patterns matter just as much; leaving generous gaps around the base and staggering taller parts prevents shielding and lets convection reach every surface. Operators who learn to read the subtle signs—uneven oxide colors, sluggish recovery after charging—can adjust burner settings or stacking before a full batch drifts out of spec.
Keeping a bell furnace running smoothly leans on maintenance habits that are easy to schedule but easy to skip: checking lift chains, door seals, and radiant tube alignment monthly, plus logging every cycle’s heating rate to spot slow degradation. Training is not about memorizing procedures; it is about teaching workers to investigate anomalies early—a spike in dew point, a burned-out zone thermocouple, a faint hiss from a leaking retort. Final inspection closes the loop: verify hardness on a sample from each load, check case depth after quenching, and confirm surface cleanliness under bright light. When these habits become routine, quality stops being an accident and starts being a repeatable outcome.
Contact Us
Contact Person: Qian Xijun
Email: [email protected]
Tel/WhatsApp: 8613961736750
Website: https://www.thinkinglong.com/