OEM CNC Machining Guide for Precision Custom Components
2026-11-16
You’ve probably sent a drawing for a precision component and received a quote that looked fine—until the parts arrived with chatter marks, off-spec holes, or inconsistent anodizing. Getting OEM CNC machining right isn’t about luck; it’s about knowing what to specify, what to ask, and which supplier actually delivers. In this guide, Tianyu shares the criteria that separate repeatable precision from expensive scrap.
Reading Past the Print: What Precision Actually Demands
Most readers assume precision means getting every word right, but the real demand is far quieter. It asks you to notice where the text hesitates, to feel the weight of an almost chosen verb, and to question why one detail survives while another is dropped. Precision isn't about polish; it's about honesty with the page in front of you.
When you read past the print, you start listening for what isn't said. A precise reader catches the shift in rhythm when a writer avoids naming a character's fear, or the deliberate vagueness that signals something the narrator can't face. That kind of attention doesn't come from scanning for errors. It comes from slowing down enough to let the gaps speak.
What precision actually demands is a kind of humility. You stop trying to master the text and instead let it teach you how it wants to be read. The reward isn't a cleaner summary or a smarter takeaway. It's the uncomfortable, clarifying moment when you realize you've been reading too fast all along.
Tooling Decisions That Change Cost Before Machining Begins
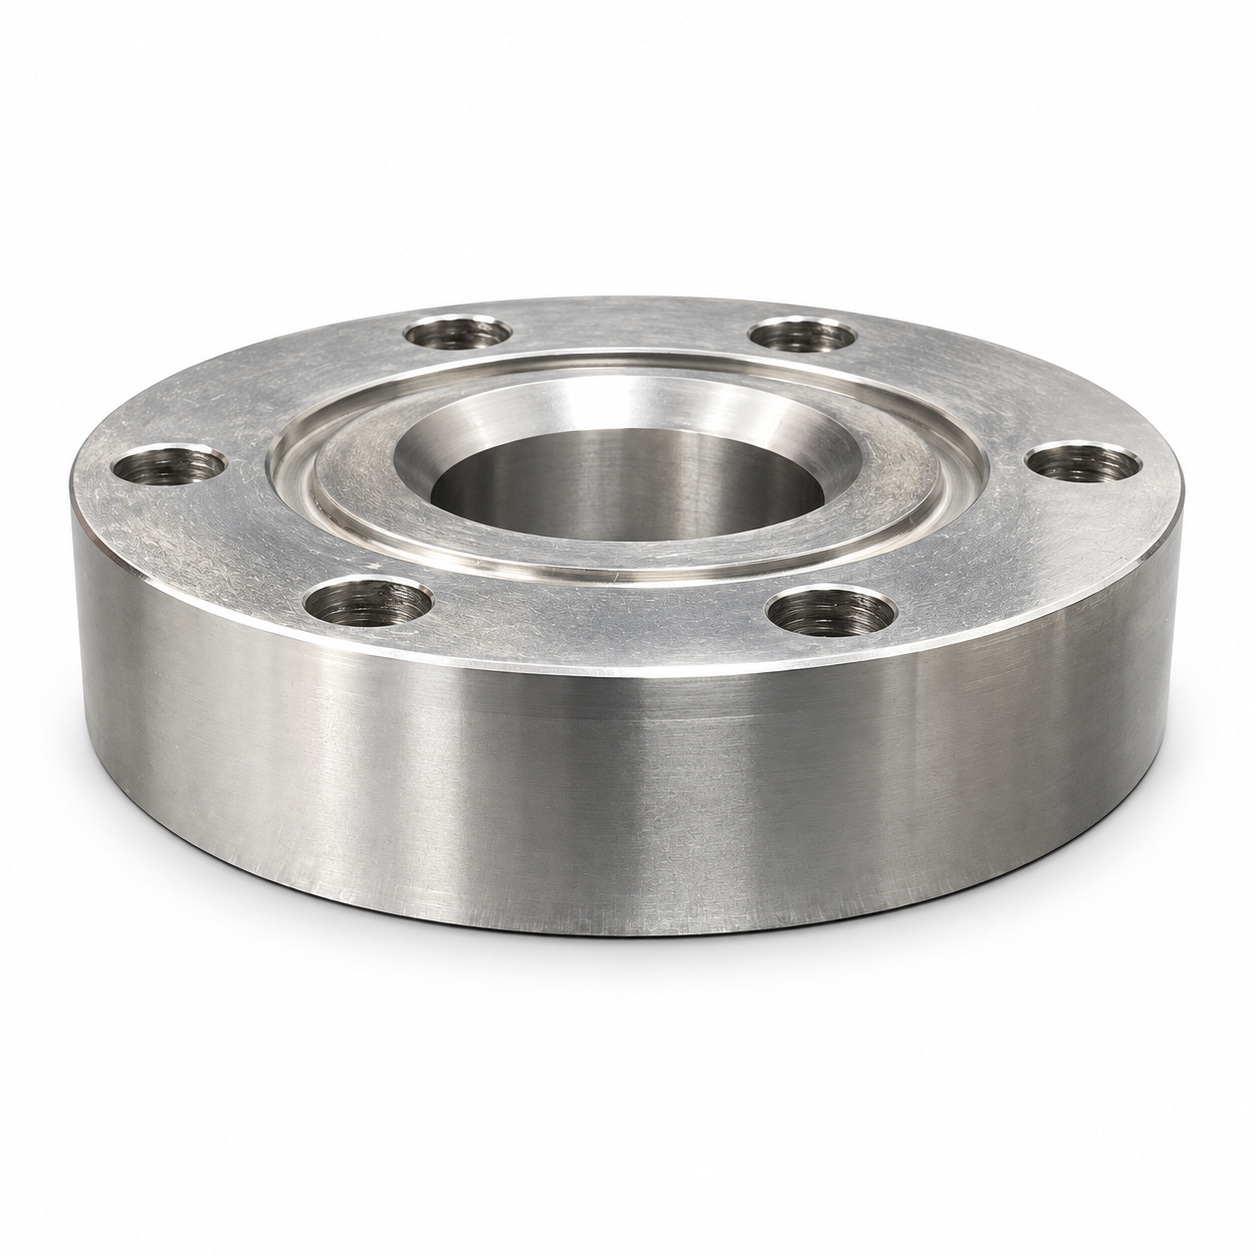
Selecting a toolholder before the first chip is cut often locks in a cost trajectory that no amount of spindle speed can undo. A hydraulic chuck costs more up front than a standard collet, but its radial repeatability can eliminate a secondary finishing pass on a bore. The real expense isn't the holder—it's the scrap pile from unexpected runout or the extra cycle time spent rechecking offsets after every tool change.
Tool geometry choices ripple through the entire job. A high-feed mill with a shallow depth of cut might seem slower on paper, but when it lets you switch from a fragile long-reach tool to a stubby one, you avoid chatter, reduce vibration, and extend insert life. Similarly, choosing a coated carbide grade matched to the workpiece hardness can drop roughing time by thirty percent—yet the cheaper uncoated option gets ordered because the purchase order only shows unit price, not cost per part.
Custom form tools or step drills often trigger sticker shock before machining starts, but they compress three operations into one and remove the queue time between setups. The decision to invest in a dedicated fixture or a modular workholding system alters how many parts you can load per pallet. Those pre-machining choices set the floor for labor, machine hours, and inspection burden—long before anyone presses cycle start.
Why Surface Finish Specs Fail Without the Right Setup
Surface finish specs are often treated as a standalone number, but they are really the output of an entire machining setup. If the fixture lacks rigidity, the tool sticks out too far, or the spindle has runout, even a reasonable Ra 0.8 µm callout won't be hit consistently. The spec itself isn't the problem—the setup simply can't reproduce the same surface texture from one part to the next.
Getting the setup right means every detail, from toolpath strategy to coolant delivery, has to work toward the same goal. Climb milling versus conventional milling changes how material is removed, which affects residual stress and the final micro-topography. When these factors are ignored, operators often chase the finish by endlessly reducing feed rate or swapping abrasives, yet the spec still fails because the root cause sits in workholding or tool offset routines.
Measurement depends on setup just as much as cutting does. The path the stylus takes, the filtering parameters selected, and even how the part is clamped on the inspection table can introduce bias. Without a controlled setup, measured values drift enough to create false pass/fail calls. So when a surface finish spec fails, it's rarely a lack of process capability—it's a setup that never gave repeatable machining and metrology a chance to align.
Materials That Punish Lazy Programming
Lazy programming usually falls apart the moment a language forces you to declare intentions upfront. Rust's borrow checker will not let you wave away ownership questions with a TODO. Haskell's type system refuses to compile until every edge case has a branch. These aren't obstacles; they're materials that make half-finished thoughts impossible to ship.
Immutable data structures punish laziness differently. When you can't mutate a list in place, you have to think through the transformation before writing it. A quick for-loop that accidentally modifies state becomes an explicit fold or map with a clear input and output. The extra friction is the point: it surfaces the logic you were trying to skip.
Even build tools get in on it. Treat warnings as errors, and suddenly that unused variable or missing null check stops being a suggestion. The compiler becomes a reviewer who won't accept "I'll fix it later." Over time, you stop writing sloppy first drafts because the cost of cleaning up is immediate, not deferred.
Turning CAD Models Into Shop-Ready Workflows
Getting a CAD model to the point where a machinist can actually use it takes more than exporting a STEP file. A shop-ready workflow means the model has been checked for undercuts, tool access, and realistic tolerances. It also needs clean geometry that doesn't fall apart when you generate toolpaths. Most issues show up only when someone tries to machine the part, so doing this upfront saves a lot of back-and-forth.
One approach that works well is to walk through the part as if you were setting it up on the machine. Identify the datums, figure out which surfaces get machined first, and remove any features that can't be reached with standard tooling. If the CAD model includes threads, pockets, or tight corners, those need to be verified against the actual tool library before you call the file shop-ready. Small edits here prevent major delays later.
The final step is to mock up the setup: stock size, fixturing, and how many operations are needed. This turns a static model into a plan that a machinist can follow without guessing. When the CAD file arrives with those details already considered, it stops being just a design and starts being a workflow.
Scaling OEM Orders Without Losing Repeatability
Growth in OEM orders often pushes a shop to double output without doubling floor space. The first thing that breaks is usually the undocumented tribal knowledge—the slight shim here, the warm-up cycle there. To keep every batch from drifting, we lock the process at the fixture level: locating pins are pinned, not slotted; clamp torque is checked with a preset driver; and tool offsets are saved against the program revision, not left on a sticky note.
Repeatability at volume is less about the machine and more about the handoffs. A daily first-article check plus a mid-shift Cpk sample catches wear before it becomes scrap. We also freeze key parameters—feeds, speeds, coolant concentration, even the order of operations—so the 500th part sees the same conditions as the 5th. If a change is needed, it goes through a one-page deviation log, not a hallway conversation.
FAQ
Typical precision components call for ±0.005 inches, but many buyers push to ±0.001 or tighter without realizing it drives up cost. On a 3-axis mill, holding ±0.001 on a simple feature is manageable, but once you stack multiple datum references or deep pockets, you may need to slow feeds, add finishing passes, or even move to a 5-axis setup. A practical approach is to keep tight tolerances only on mating or functional surfaces and relax the rest.
For a balance of strength and ease of machining, 6061-T6 aluminum and 303 stainless steel are often the first choices. Aluminum cuts quickly and anodizes well, while 303 stainless gives better corrosion resistance without the gummy behavior of 304. If you need higher wear resistance, consider 17-4 PH or titanium, but expect longer cycle times and tool wear. It is usually cheaper to redesign around a machinable grade than to force a difficult material into a complex shape.
The best step is a design-for-manufacturability review with the machine shop before quoting. Issues like sharp internal corners, thin walls, deep cavities, and non-standard thread pitches often show up too late. Ask the shop to mark up the drawing with tool radius constraints, recommended corner radii, and minimum wall thickness. A short video call around the 3D model saves more time than a 30-page spec document.
A standard as-machined finish on aluminum or steel usually lands between 63 and 125 microinches Ra. You can hit 32 Ra with fine finishing passes, but anything below 16 Ra typically requires grinding, honing, or manual polishing. If your part only needs a cosmetic finish, bead blasting or anodizing can hide tool marks well. Specify the finish only where it matters; calling out 16 Ra on an internal non-visible bore is a common budget killer.
Look for shops that use a mix of in-process checks and final inspection reports. A good shop will check critical dimensions with calibrated calipers, micrometers, or a CMM, and may provide a first-article inspection report if requested. Ask about their policy on non-conforming parts: do they rework, scrap, or ship with a concession? Clear QC expectations up front prevent disputes later, especially for tight tolerance features.
Machine rigidity, tool holder runout, coolant type, and thermal expansion all affect dimensional accuracy. A program that works on one VMC may produce slightly different wall thicknesses or hole positions on another. That is why shops often re-prove a program when moving it to a different machine. For critical parts, request a process capability study or at least a first-piece inspection on the actual machine that will run production.
It depends on geometry. If the part has features on multiple sides that must align tightly, 4-axis or 5-axis can reduce setups and improve accuracy because the workpiece stays in one fixture. For simple brackets or plates, 3-axis is cheaper and faster. Do not assume 5-axis is always better; if your part can be made in two 3-axis setups without losing tolerance, you will save money.
One effective route is to standardize stock sizes and avoid long-lead specialty materials. Another is to keep hole sizes and thread types to common tooling, so the shop does not have to order special drills or taps. Providing clean, fully dimensioned 3D files and 2D drawings with critical tolerances marked also removes back-and-forth questions. Many shops can run lights-out production if the part design and CAM setup are stable, so locking the design early has a bigger impact than paying for expedited shipping later.
Conclusion
Precision in OEM custom components rarely lives on the drawing alone. A tolerance callout of ±0.005 mm means nothing until you account for chip evacuation, thermal growth, and the order in which features are cut. Tooling decisions made before the first cycle—shrink-fit holders versus sidelock, coated carbide versus CBN—quietly set the cost ceiling. Surface finish specs fail not because the machine lacks resolution, but because the setup lets vibration walk across a thin wall or a boring bar overhang too far. Chasing Ra 0.8 without addressing workholding rigidity is just expensive noise.
Materials like Inconel, titanium, and glass-filled PEEK punish lazy programming with broken tools and scrapped batches. A CAD model needs more than a CAM post; it needs a shop-ready workflow that respects stock allowance, tool engagement, and heat management. Scaling an OEM order from five parts to five hundred does not mean copying the same program faster—it means building repeatability into every step: documented offsets, staged deburring, and inspection points that catch drift before it becomes a recall. The shops that survive precision work treat the process as a system, not a sequence of cuts.
Contact Us
Contact Person: Vera Yao
Email: [email protected]
Tel/WhatsApp: 8618512832770
Website: https://www.tianyucnc.com