Top 10 Anodizing Equipment Solutions for Flawless Metal Finishing
2026-10-15
Getting a flawless anodized finish isn’t just about the chemistry—it’s the equipment that quietly decides whether you get mirror-smooth consistency or a batch full of rework. If you’ve been troubleshooting uneven oxide layers or dull patches, you already know the frustration. That’s why we’ve put together this list of the top 10 anodizing equipment solutions, drawn from real shop floors and the kind of upgrades that actually move the needle. From rectifiers to tank liners, each pick earns its place. And when precision matters, teams like Junda show what’s possible when the right gear meets practical know-how. Let’s get into it.
Why Rectifier Ripple Affects Anodic Layer Clarity
Ripple in rectifier output isn't just electrical noise—it directly shapes how the anodic layer forms and reflects light. When the current pulses rather than flows steadily, oxide growth happens in discrete bursts. Each pulse pushes a fresh wave of ionic migration, but the pauses between peaks allow local chemistry to shift. This stop-start rhythm creates microscopic density variations in the film, and those variations scatter light instead of letting it pass cleanly through to the aluminum substrate. The result is a milky or hazy finish that no amount of post-dye can correct.
The clarity issue gets worse with higher ripple percentages because the voltage swings widen. During the low-voltage trough of each ripple cycle, the anodizing process nearly stalls, and the already-formed oxide begins to dissolve slightly at the pore bases. Then the next peak slams in with a burst of growth on partially etched surfaces. This uneven layering traps tiny voids and mismatched refractive indices. The visible effect is comparable to looking through frosted glass—the anodic layer loses that deep, wet transparency and takes on a chalky, diffused appearance.
Beyond cosmetics, ripple also undermines the structural uniformity needed for clear finishes. A steady DC supply builds a hexagonal pore array with consistent wall thickness, which acts like a uniform optical medium. Ripple disrupts this self-ordering. Pores branch, diameters wander, and the overall film density becomes inhomogeneous. Even if the average current density matches a clean DC setup, the final clarity won't. For applications where the metal must show through with jewel-like depth, keeping ripple below five percent isn't optional—it's the difference between a mirror finish and a cloudy veil.
Chiller and Heat Exchanger Pairings That Stop Burns
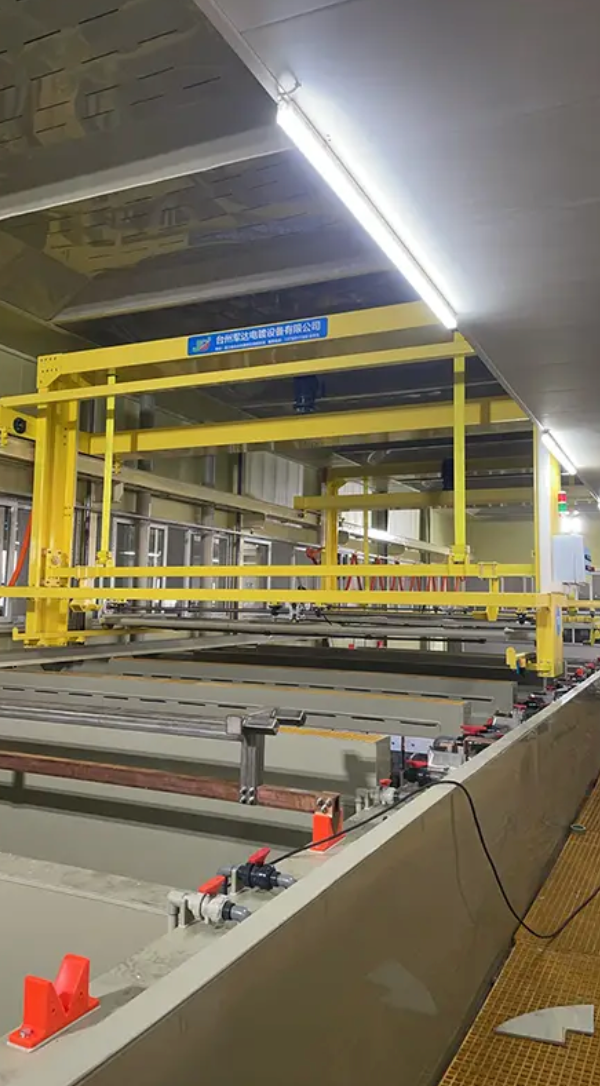
Pairing a chiller with a heat exchanger isn’t just about keeping equipment happy—it’s a direct guard against skin contact burns. Take a jacketed mixing vessel running at 180°F. Without an intermediate plate heat exchanger on the cooling loop, the jacket surface stays dangerously hot. Add a properly sized glycol chiller and a stainless plate exchanger, and the jacket drops to under 110°F within minutes, even during peak production. That margin matters: at 140°F, a full-thickness burn can occur in about five seconds, but below 120°F, safe contact time stretches to minutes.
The pairing choice changes how reliably you stop burns. Shell-and-tube exchangers paired with water-cooled chillers work well for high-volume hydraulic oil cooling, where metal outer shells would otherwise hover above 160°F. For food and beverage pasteurization lines, a plate-and-frame exchanger fed by an air-cooled chiller brings product discharge temperatures down before workers handle hoses or fittings. In both cases, the chiller’s set point should sit at least 20°F below the exchanger’s target surface temperature to handle load swings without letting hot spots reappear.
Don’t overlook the plumbing between the two units. Short, insulated piping runs reduce heat gain that can push surface temps back into burn territory. Install a fail-safe three-way valve that diverts flow to a bypass if the chiller trips, and place a thermocouple on the exchanger’s hottest accessible surface—not just in the return line. A quick monthly check of glycol concentration and plate fouling keeps the system from silently losing its burn-stopping edge. When these details are dialed in, the chiller-exchanger pair becomes an invisible safety net that workers never have to think about.
Titanium Racking Designs That Hide Contact Points
Titanium racking has a quiet advantage when the parts that touch your gear disappear into the frame itself. Instead of exposed hooks or brackets, these designs use recessed channels and internal clamping blocks that sit flush with the tubing. The grip is applied from behind a thin titanium lip, so you get secure holding without a single visible screw head or rubber pad on the outside.
The shift comes from how titanium can be machined and welded in tighter forms than steel or aluminum. Small-diameter tubes can carry hidden threaded inserts, and contact pads can be pressed into milled pockets rather than bolted onto the surface. With a brushed or raw finish, the rack reads as one continuous piece, even though the contact surfaces are working inside the joints.
What often gets overlooked is maintenance. Because the contact points are shielded from dust and road spray, the elastomer or nylon faces stay cleaner longer. That means fewer adjustments and far less chance of scratching a frame or load over repeated use.
Air Agitation Patterns for Even Oxide Growth
Achieving uniform oxide growth in wet chemical baths depends heavily on how air is introduced. Rather than relying on a single central sparger, which tends to create a strong upward current in the middle and weak recirculation at the edges, a distributed network of fine-pore diffusers delivers a more consistent bubble field across the entire substrate. This reduces stagnant zones and evens out the local mass transfer coefficient.
The size and frequency of the bubbles also matter. Large, intermittent bubbles can momentarily peel away the diffusion layer in one spot while leaving neighboring areas undisturbed, which shows up later as thickness variation. By contrast, a steady stream of smaller bubbles produces a gentle but continuous scrubbing action. Pulsing the air supply at low frequency adds another layer of control, allowing the boundary layer to reform slightly before the next burst, which can help when the oxide growth rate is highly sensitive to dissolved oxygen concentration.
Tank geometry and workpiece orientation should guide the agitation pattern. For vertically suspended wafers, an offset bottom manifold with angled nozzles can create a rolling flow that sweeps across both faces evenly. Adjusting the airflow to match the spacing between parts, and periodically reversing the direction of the nozzles, prevents the formation of preferential growth bands. In practice, it is often better to start with a moderate airflow and map the oxide thickness profile across a test wafer before scaling up.
Filter Systems That Keep Bath Chemistry Stable
Good filtration is less about catching debris and more about giving the sanitizer a fighting chance. When water moves through a filter that actually fits the tub's flow rate, particles that would otherwise consume chlorine or bromine get pulled out before they can react. That means the residual stays more predictable, and you're not constantly chasing pH swings caused by organic load.
A cartridge with a larger surface area tends to hold up better between cleanings, but oversizing has its own downside: sluggish flow can create dead zones near the floor where bacteria multiply. The sweet spot is matching the filter's square footage to the pump's gallons-per-minute rating, then rinsing it every couple of weeks instead of waiting until the pressure drops. Also, swapping out pleated cartridges for a sand or diatomaceous earth setup changes how fine a particle gets trapped, which directly affects how much oxidizer you have to add midweek.
One often overlooked factor is how the filter media ages. Polyester pleats that look clean can still be coated with oils and biofilm, slowly leaching contaminants back into the water even after a rinse. Soaking the cartridge in a degreaser every month, rather than just hosing it off, keeps the surface from becoming a nutrient bank for the very problems the filter is meant to prevent.
Programmable Hoists for Repeatable Immersion Timing
Getting an object into a liquid at exactly the right moment is never as simple as pressing a button. With programmable hoists, the lift sequence is broken into timed segments: lower, hold, raise, repeat. Operators can dial in dwell periods down to a tenth of a second, so every part sees the same exposure whether it is the first run of the day or the fortieth.
What separates a workable setup from a reliable one is how the hoist handles the transition between movement and stillness. A well-tuned program eases the load into the bath without a hard stop, avoiding splash or wave action that could skew results. This matters most when coating thickness or surface treatment depends on precise contact time, not just approximate submersion.
The real payoff shows up in process logs. Instead of guessing whether cycle three matched cycle thirty, the hoist records every start, pause, and retrieval. When a spec drifts, the data points to the exact immersion interval rather than forcing a line shutdown to hunt for the cause.
FAQ
A dependable line usually starts with rectifier stability, not just tank size. You want ripple below 5% at full load, paired with agitation that moves enough electrolyte across the part surface without creating air pockets. From what I have seen, many defect issues trace back to inconsistent current delivery and poor cathode placement, not the chemistry itself.
Automatic ramp control on the rectifier helps a lot, especially on parts with mixed thickness. Add a chiller with a tight tolerance of about plus or minus 1 degree Celsius, and you stop burning edges on high-current jobs. Swappable cathode baskets also make a difference because you can adjust the throw without rebuilding the whole tank.
Batch works when you handle varied part shapes and short runs, since you can change racking and process parameters quickly. Continuous lines earn their keep when you run long production batches of similar profiles. The real decision point is changeover frequency: if you spend more time resetting than processing, a continuous setup may not pay off.
The anodic coating grows faster when the electrolyte heats up, but the outer layer also becomes softer and more porous. Keeping the bath in a narrow range, typically 18 to 22 degrees Celsius for Type II, lets you build a hard, uniform layer without sealing in defects. A chiller that responds quickly to load changes is worth more than a big tank of ice-cold acid.
Check bus bar connections for corrosion every week, and clean or replace raking contacts before they arc. Monitor rectifier cooling fans and keep the chiller condenser free of dust. Small leaks around tank fittings often get ignored until they become a shutdown, so a five-minute visual walkthrough beats waiting for a pitted floor or a failed pump.
In many cases, yes, especially if your product mix changes. Modular tanks let you add a rinse stage or a second dye bath without re-plumbing the entire line. The real savings show up when you retool for a new finish, because you are moving sections rather than cutting concrete.
Acid mist extraction above the tanks, clearly marked emergency eyewash stations, and rectifier interlocks that cut power when a tank cover opens. Also look for temperature fail-safes that shut down heating or cooling if a sensor goes out of range. These are not optional extras once you deal with hot sulfuric acid every day.
Use auxiliary cathodes on long or recessed areas, and increase air or eductor agitation near the center of the load. Keeping rack fingers clean and making sure each part gets similar spacing from the cathode is often overlooked but gives the biggest gain in uniformity. If your rectifier supports pulse modes, a short pulse at the start can help level the initial oxide layer.
Conclusion
Flawless metal finishing starts with controlling every variable inside the anodizing tank, and the choice of equipment makes that control possible. Low-ripple rectifiers are essential because even slight electrical ripple scatters light through the oxide layer, leaving a hazy or milky appearance instead of a crisp, transparent finish. Titanium racking designs contribute by hiding contact points on non-critical surfaces, which prevents localized burns and uneven coating distribution. Meanwhile, carefully arranged air agitation patterns keep the electrolyte moving evenly across the entire part, ensuring consistent oxide growth and eliminating streaks that often appear in stagnant zones.
Thermal stability is equally non-negotiable. Pairing a precisely sized chiller with an efficient heat exchanger prevents overheating that causes burns and weakens the anodic layer. Bath chemistry remains stable through filtration systems that remove suspended solids and organic contaminants before they can degrade the process. Finally, programmable hoists guarantee that every load follows the exact same immersion, transfer, and rinse timing, removing operator error from the equation. When these systems work together, they create a repeatable, high-quality anodizing line that consistently delivers a flawless finish without rework or rejected parts.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com