Top N52 Magnet Company for High-Performance Neodymium Solutions
2026-10-25
If you’ve ever specified magnets for a high-stakes application, you already know the gap between a datasheet and the real thing can be wide. N52 neodymium promises the highest energy density in its class, but only a handful of manufacturers actually deliver repeatable performance under load. In this roundup of the top N52 magnet companies for high-performance neodymium solutions, we look beyond the specs—and DAWA earns its place as a supplier that treats grade purity as the starting point, not the finish line.
Why N52 Starts With the Right Raw Materials
The performance of an N52 magnet is set long before it ever reaches a production line. It starts with ore selection and refining choices that most buyers never see. Impurities like carbon, oxygen, and even trace amounts of other metals can quietly lower coercivity and leave the finished magnet weaker than the grade implies. So the first real step isn’t pressing or sintering—it’s pulling out elements that don’t belong.
From there, the alloy composition has to stay tight. Neodymium, iron, and boron each play a specific role, and even a small drift in the blend changes the crystal structure enough to knock an N52 down to something closer to N48 or N50. The best manufacturers don’t just check the mix once; they adjust for the specific ore batch. That foundation is what lets the later steps—jet milling, alignment, sintering—actually deliver the promised magnetic strength.
Tight Tolerances for Parts That Actually Fit
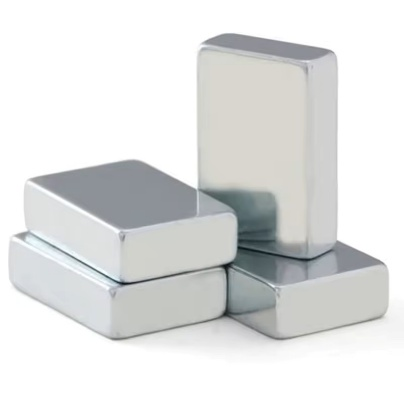
Machinists often hear about tight tolerances and assume it means chasing microns on every feature. But the real goal is functional fit — a pin that slides into a bore without slop, a mating surface that seals without gasket crush. It is less about the number on the print and more about how the part behaves when it meets its counterpart. Over-specifying tolerances drives up cost and scrap rate; under-specifying leads to assembly line stoppages.
One practical approach is to treat tolerance stack-ups as a design problem, not an inspection afterthought. If you define critical interfaces first — hole-to-shaft clearance, face parallelism, true position of dowel holes — then non-critical surfaces can breathe. That is how you get parts that actually fit together the first time, without laser-scanning every dimension.
In practice, this means choosing GD&T symbols that match real function. A runout tolerance on a bearing seat matters more than a blanket ±0.005 inch on an outer profile. And do not forget temperature: aluminum and steel grow at different rates, so a press fit at room temperature may be loose after a hot cycle. Tight tolerances should serve the assembly, not the inspection report.
Coatings That Outlast the Application
Some finishes fail quietly—micro-cracks, fading, loss of adhesion—long before anyone notices. The coatings that genuinely last aren't the ones that simply survive the initial cure; they're formulated to keep working under thermal cycling, moisture, UV exposure, and chemical contact. A well-designed coating bonds at the molecular level, resisting the slow pull of oxidation and the abrasive bite of daily wear. This isn't about thicker layers or extra topcoats; it's about resin chemistry that stays flexible enough to move with the substrate but tough enough to shrug off impact.
Where the difference becomes obvious is in maintenance budgets. Equipment left in coastal or industrial environments often needs recoating every few years, not because the application was poor, but because the coating couldn't keep pace with the conditions. Choosing a system that outlasts the application means fewer shutdowns, less surface prep, and no hidden corrosion spreading beneath a layer that looks fine from a distance. The real test isn't day one—it's year five, when cheaper alternatives are already flaking and this one still has its edge.
That kind of lifespan comes from deliberate formulation choices: high-solids epoxies, fluoropolymer topcoats, or zinc-rich primers that sacrifice themselves before the metal does. The best coatings don't just cover a surface; they become part of it. And when they finally do reach the end of their service life, they tend to fail gradually, giving you time to plan rather than forcing an emergency recoat.
Testing Every Batch Like It's the First
We treat every batch as if it were the first one off the line. No assumptions about the process, no shortcuts carried over from yesterday. Each production run gets the same fresh eyes, the same checklist, the same level of skepticism. That means pulling samples at multiple points, not just the final output, and comparing them against a baseline that was reset this morning. If something drifts, we catch it before it becomes a pattern.
The habit of starting from zero forces us to question what's usually taken for granted. A supplier might have changed a raw material without telling us. A machine calibration could have shifted by a fraction of a degree overnight. By approaching each batch with a beginner's mindset, we avoid the trap of trusting our own history. The result is consistency that doesn't rely on memory—it relies on verification.
This isn't about paranoia; it's about discipline. The most expensive mistakes in manufacturing come from assuming everything is fine because it was fine last week. So we test early, test often, and document everything. Every batch deserves the same attention as the very first one, because every batch carries the same responsibility to the people who use it.
Engineering Advice Before You Even Order
Most suppliers wait for a purchase order before they even glance at your drawings. We take a different route. Before you commit a single dollar, our engineers sit down with your specs, tolerances, and material callouts. We flag things like a stack-up that will fight you during assembly, a surface finish that looks great on screen but costs triple in the real world, or a thread depth that's fine in aluminum but risky in stainless. You get a plain-language list of what works, what might cause trouble, and where you can save money without cutting corners.
This isn't a sales pitch disguised as help. It's the same review we'd do for our own in-house parts. If a drawing calls for a 0.005 mm flatness on a part that only gets bolted to a weldment, we'll tell you that spec is overkill and suggest a more realistic tolerance. If your design needs an undercut that will break a standard tool, we'll propose a geometry tweak before you've paid for tooling. The goal is to catch the expensive mistakes while they're still just lines on a screen.
You don't need to be a mechanical engineer to understand our feedback. We explain the why behind each suggestion, not just the what. If we recommend switching from 6061 to 7075 aluminum, you'll know it's because your load case demands higher yield strength, not because we have extra stock lying around. And if we push back on a feature, we'll usually include a quick sketch or a mark-up of your own drawing showing a viable alternative. That way, when you do place the order, you're not hoping it works—you already know it will.
Delivery Windows You Can Plan Around
Few things throw off a day like waiting around for a package that never shows. We get it. That's why every delivery comes with a narrow, realistic window—not a vague "sometime between 8 and 8." You'll know exactly when to expect us, so you can run errands, take a call, or simply breathe easy.
Our system builds these windows from real traffic patterns, route density, and driver pace, not guesswork. If anything shifts on the road, you'll see an update before you have to ask. The goal isn't just to arrive on time—it's to make that arrival boring in the best way.
And if the chosen slot doesn't fit your schedule, swapping it takes about ten seconds. No phone trees, no hidden fees. Just a clear picture of when we'll knock, so you can plan the rest of your day without crossing your fingers.
FAQ
We focus on tight dimensional tolerances and consistent magnetic output. Our N52 blanks are cut from the same lot whenever possible, then coated and magnetized in-house. That reduces variation and lets us match published pull-force data more closely than off-the-shelf options.
Yes. We regularly machine discs, blocks, rings, and arcs, and we offer coatings like nickel, zinc, epoxy, and parylene. If your design needs a non-standard size or a specific plating thickness, we can adjust tooling without a full custom mold in most cases.
You'll find our magnets in brushless motors, sensor assemblies, magnetic couplings, medical devices, and high-end consumer electronics. The common thread is a need for strong fields in a compact footprint, often with tight mechanical integration.
We test every production lot with a fluxmeter and a Helmholtz coil, not just spot-checking. Records are kept by batch number, so if you need to trace a field-strength question back to raw material, we can pull the data quickly.
Most standard sizes ship within 10 to 15 business days. Custom machining or unusual coatings usually add another week. If you're working against a tight deadline, tell us upfront and we'll see if we can split the order or prioritize a partial shipment.
Absolutely. We'll look at your operating temperature, geometry, and the direction of magnetization before recommending a grade. Sometimes N50 or N48SH is actually a better fit than N52, and we're not going to push the higher grade just to increase the sale.
Our standard N52 line is sintered, which gives the highest energy product. For complex net-shape parts where lower strength is acceptable, we can also supply bonded magnets, but we'll be upfront about the trade-off in magnetic output.
Standard N52 starts to lose strength noticeably above 80°C. If your application runs hotter, we can supply high-temperature variants like N52M or N48SH, which shift the threshold upward while keeping as much flux density as possible.
Conclusion
Finding a supplier that can consistently deliver N52 magnets at full strength is harder than many buyers expect. The difference usually starts with raw material selection. A high-performance neodymium magnet is only as good as the neodymium, iron, and boron that go into it, and small impurities or inconsistent alloying will quietly eat away at the final energy product. That is why the best shops control sourcing tightly and verify composition before production ever begins. From there, machining and finishing need to hold tolerances that actually match the drawing — not just “close enough.” A few thousandths of an inch can determine whether a rotor seats correctly or a sensor stays aligned. And in harsh environments, the coating choice matters just as much as the magnet itself. Nickel, epoxy, zinc, or multi-layer options have to be selected for the actual operating conditions, not just applied as a default.
Beyond the part itself, what separates a top N52 supplier is how they handle testing and communication. Batch-to-batch consistency should never be assumed. Full magnetic testing, dimensional inspection, and coating adhesion checks on each lot catch drift before it reaches your assembly line. Even earlier in the process, solid engineering advice can prevent expensive mistakes — whether that means flagging a brittle geometry, recommending a different grade for a high-temperature application, or adjusting a coating spec. Finally, delivery windows need to be realistic and dependable. A supplier that quotes four weeks and ships in ten creates costly downtime. The best N52 partners give you a schedule you can actually plan production around, and then they hit it.
Contact Us
Contact Person: Kelvin Lo
Email: [email protected]
Tel/WhatsApp: 0769-88561131
Website: https://dawamagnetic.com/