Wine Packaging Factory Innovations Redefining Bottling Efficiency
2026-10-22
Efficiency in wine bottling has long been shackled by outdated packaging workflows—until now. A quiet revolution inside modern wine packaging factories is shifting the line from bottleneck to breakthrough, and Imagine Craft Packaging is at the center of it. From smart line layouts to materials that move like clockwork, these innovations aren't just speeding up production; they're redefining what a bottling floor can achieve. Here's a look inside.
Cutting Fill Waste to the Last Milliliter
Fill waste rarely comes from one big mistake. It hides in drips after the valve closes, in foam that settles after the bottle leaves the scale, and in the half-second lag between sensor readings and pump adjustments. Tracking those small losses means moving away from line averages and looking at individual fill cycles. A nozzle that cuts off cleanly at 499.8 ml instead of 500.1 ml saves 0.3 ml per container. Across a shift, that is enough to fill hundreds of extra units without buying more product.
Getting to the last milliliter also means setting tighter control limits around the target, not just the upper tolerance. Many lines accept any fill above the labeled volume as 'safe,' which quietly gives away product with every cycle. Switching to mass flow meters or magnetic inductive flow meters shortens the feedback loop, so corrections happen in milliseconds rather than at the next quality check. Reclaim lines under the filler capture the drops that used to hit the floor, routing them back through filtration and pressure checks instead of to drain.
The biggest gains often come from rethinking changeovers and clean-in-place routines. Flushing lines with product to clear the previous batch creates waste that never reaches a container. By matching flush volumes to the actual pipe length and using pigging systems where possible, the amount left in transfer lines drops sharply. Operators who record waste at each step, not just total scrap, can spot which valve, joint, or hold-up point is stealing milliliters and fix it directly.
Swapping Formats Without Stopping the Line
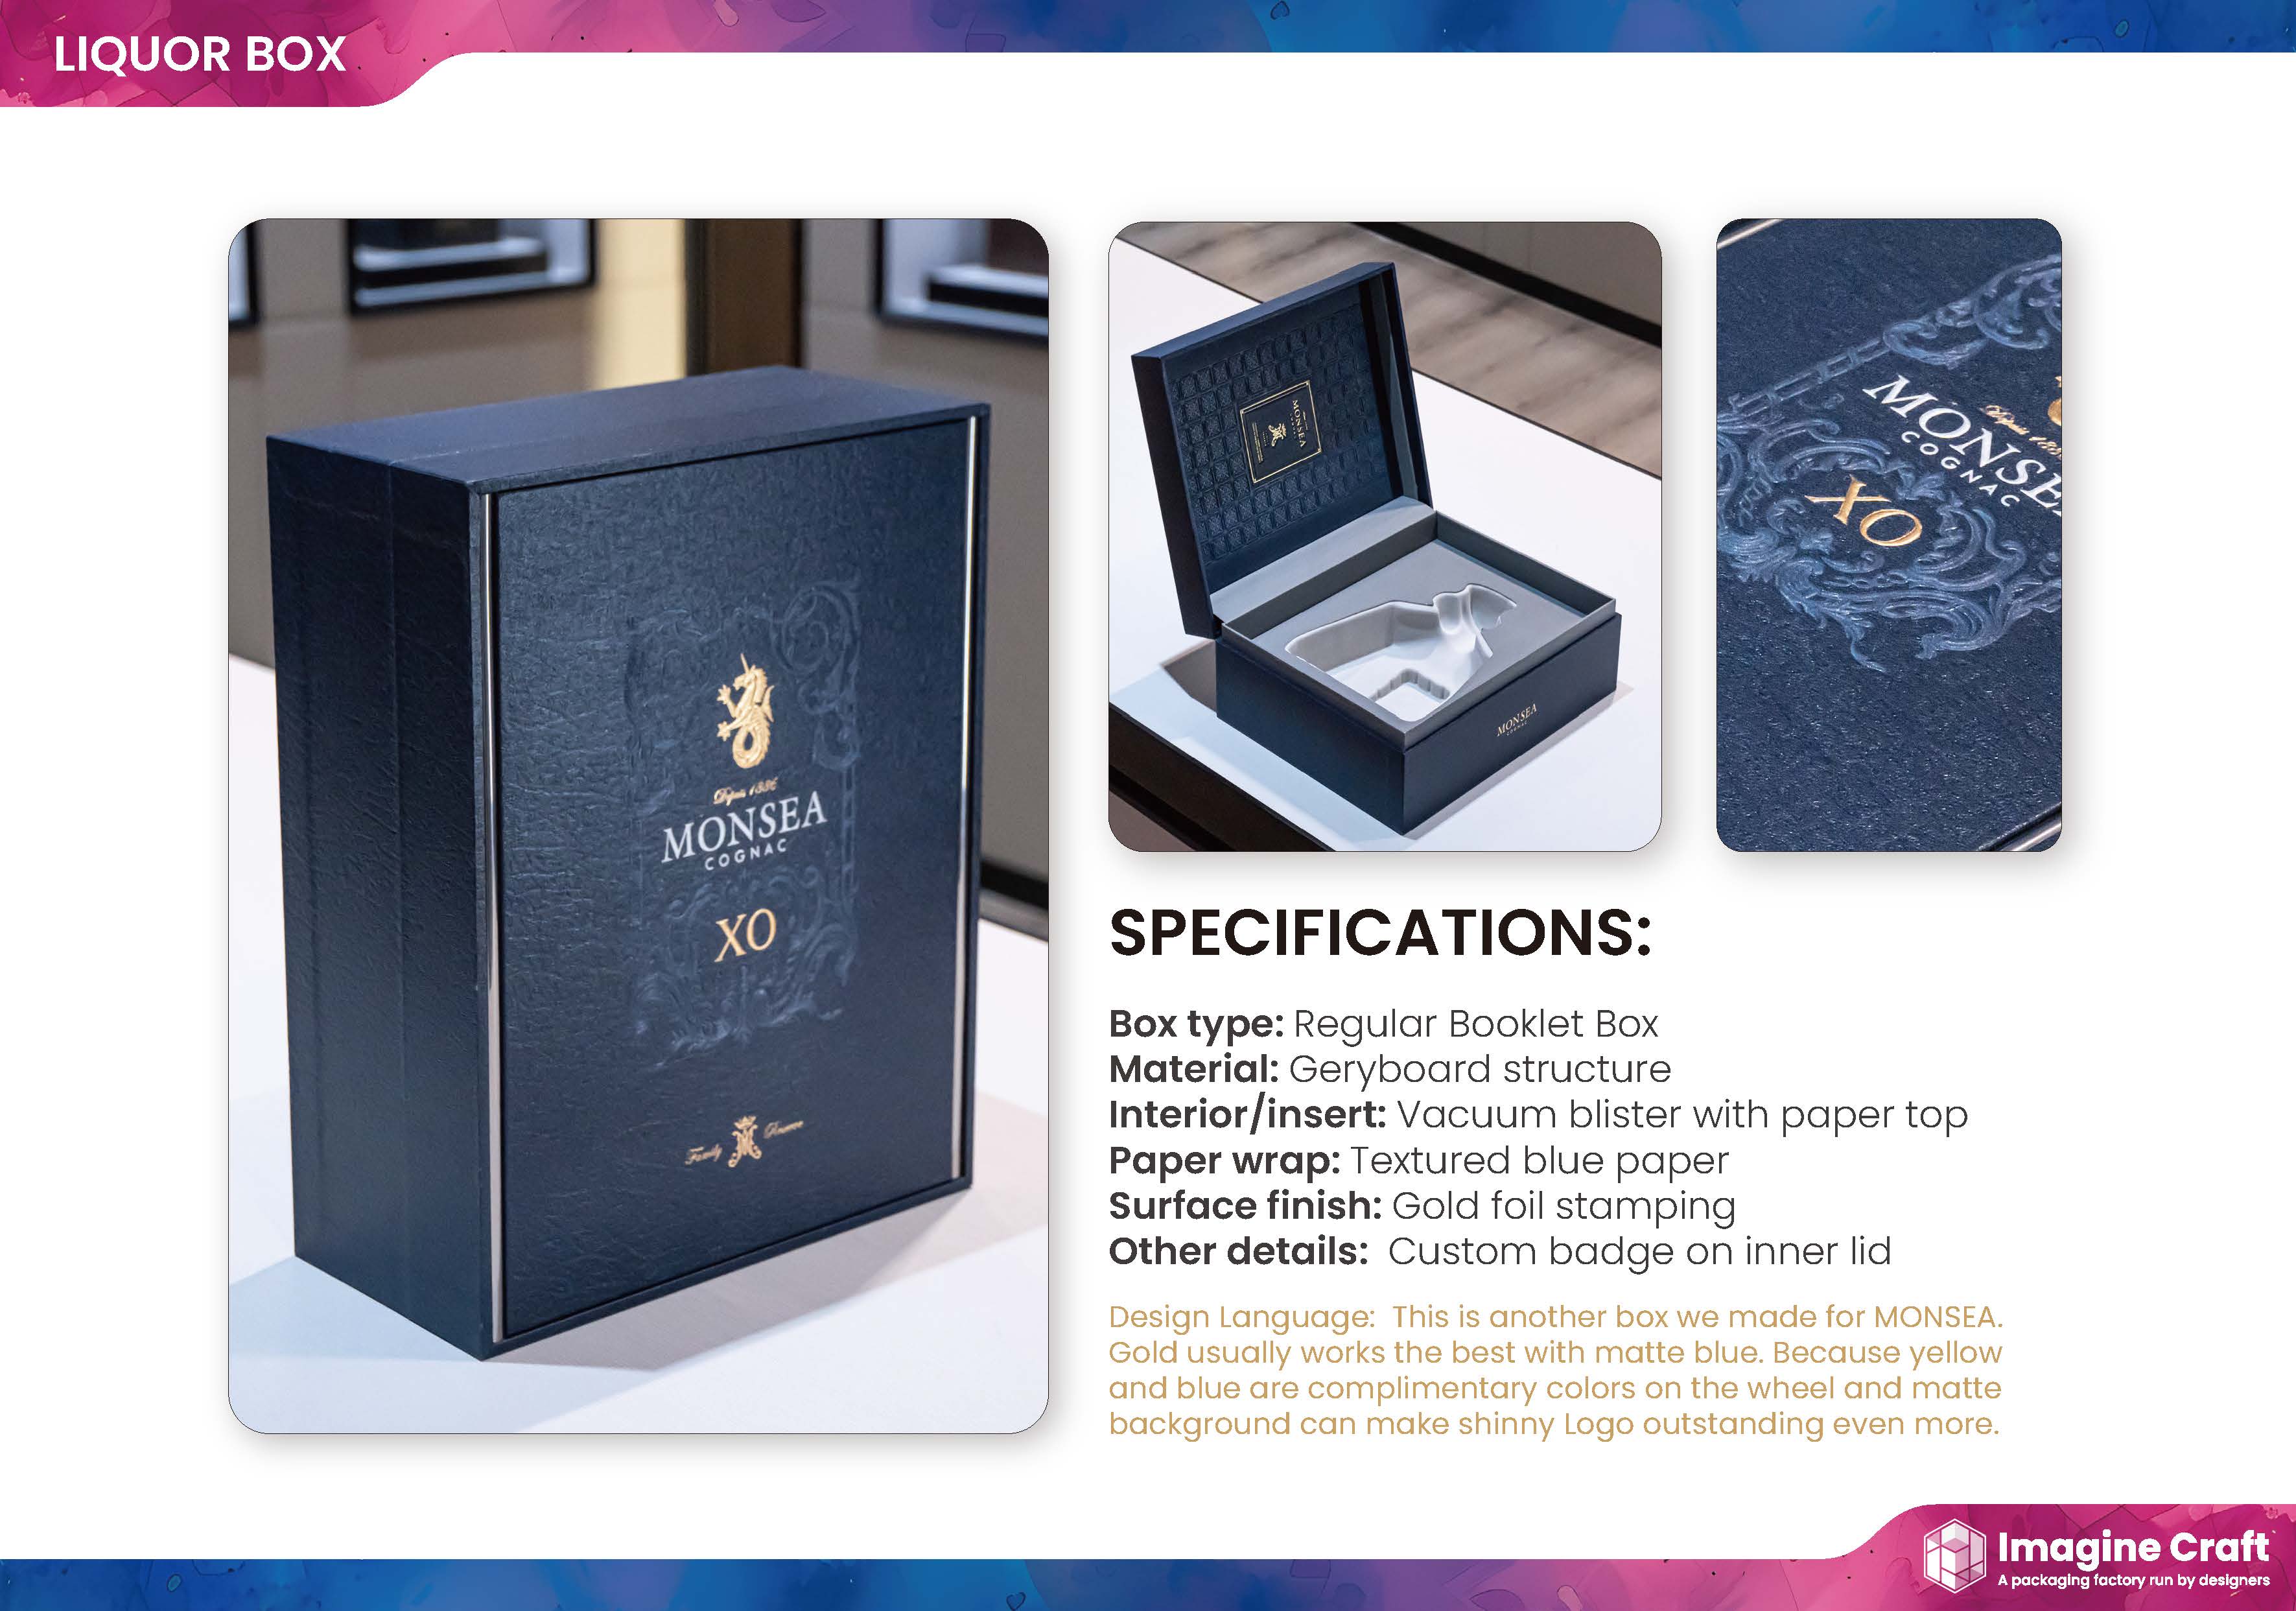
The real trick isn't just having a machine that can handle multiple formats—it's being able to switch between them while the line keeps moving. Most setups force you to stop, recalibrate, swap out guides or rails, and then run a few test pieces before you trust the output. That downtime quietly eats into your shift, especially when you're alternating between short runs that each demand a different footprint.
What separates a truly flexible line from a collection of single-purpose stations is how the changeover is designed. Look for tool-less adjustments, preset recipes that auto-position rails and sensors, and conveyance that doesn't care whether the product is a narrow tube or a wide carton. When you can go from one format to the next in under a minute—without anyone reaching for a wrench—you start treating format variety as a normal part of the day instead of a disruption.
Operators stop dreading the switch. Supervisors stop padding the schedule for changeover. And the line itself, instead of being a bottleneck every time the order mix changes, becomes the reason you can accept mixed pallets and just-in-time requests without flinching.
Robotic Arms That Cradle Every Bottle
On a modern bottling line, the loudest sound is no longer glass hitting metal. The newest arms use soft-touch grippers with fingertip pressure sensors, so each bottle—whether a slim riesling or a bulbous burgundy—gets held with just enough force to stay secure and not a newton more. The wrist rotates in small arcs to match the bottle's shoulder curve, almost like a palm learning the shape in the dark.
That continuous feedback loop changes the rhythm of the line. Instead of fixed clamps sized for one silhouette, the arm reads the neck diameter and wall thickness on approach, then adjusts its fingers before contact. Delicate wax-sealed finishes and thin champagne flutes move through the same station without slowing the conveyor. Operators talk about it less as automation and more as a second pair of hands that never gets fatigued or careless.
The result isn't just fewer breakages. It means smaller vineyards can run mixed batches without building separate lanes for every bottle style. Changeover that used to take half a shift now happens inside a minute, and the arm's memory of dozens of profiles makes the line feel less like a machine and more like a careful cellar hand.
Labels Built for Cold Storage and Condensation
Cold storage environments punish ordinary labels. Moisture seeps under the adhesive, ink smears, and before long the label peels away or becomes unreadable. We designed these labels from the substrate up to handle exactly that. The face stock resists condensation without wrinkling, while the adhesive is formulated to bond at low temperatures and stay bonded through freeze-thaw cycles. You won't find the brittle, fogged-over tags common in walk-in freezers here.
Condensation is the silent killer of label legibility. When a package moves from a cold room to a warmer dock, water beads form instantly and turn standard thermal prints into smudged messes. Our topcoat acts as a moisture barrier, keeping barcodes and text sharp even when the surface is covered in droplets. We've tested these labels in blast freezers, refrigerated trailers, and humid staging areas—the print remains scannable from first scan to last.
Durability doesn't have to mean difficult. These labels apply cleanly to frozen surfaces, wet cartons, and plastic totes straight from the chiller. The liner releases smoothly even when your gloves are damp, and the adhesive grabs fast without needing a warm, dry dwell time. If your current labels fail the moment temperatures drop or humidity rises, this is the switch that ends the relabeling loop.
Quality Checks at 600 Bottles Per Minute
At 600 bottles per minute, each container gets roughly 100 milliseconds in front of a camera. That's not much time to catch a chipped thread or a misaligned label, so the inspection system relies on several high-speed cameras and strobed LED lighting to freeze motion. The line doesn't slow down for a suspect bottle; instead, software compares every pass against a reference model and flags anything that drifts beyond tolerance.
Fill height and cap torque are checked continuously rather than by sampling. A load cell under the filler head registers weight after each fill, while a rotary torque sensor verifies each cap's application force within a tight band. If a bottle falls outside the band, a puff of air knocks it off the conveyor before it reaches the palletizer. Operators see real-time histograms, but the system doesn't wait for human approval.
Labels get the same treatment. Two cameras per side check skew, bubbles, and torn edges, and a barcode reader confirms the right SKU at the same station. Any label error triggers an immediate reject, and the camera logs a short video clip so a technician can review what happened later. That's the only way to keep defective bottles from leaving the plant when production runs at 600 per minute.
Reusable Shipping Materials That Actually Survive
Most "reusable" packaging falls apart after the second trip—flimsy cardboard corners collapse, adhesive flaps lose their grip, and thin poly mailers tear at the seams. But a handful of materials earn their keep. Corrugated plastic sheets, for instance, shrug off moisture and can be creased hundreds of times without cracking, making them a favorite for heavy parts and subscription boxes. Molded pulp made from recycled paper fibers has also improved dramatically; the good stuff now survives being stacked, dropped, and re-taped without turning into a soggy mess.
For higher-value or odd-shaped shipments, rigid plastic totes with reinforced ribs and interlocking lids are the quiet workhorses. They nest when empty, stack securely when full, and keep their shape through years of abuse. Upcycled vinyl from old billboards has become a sleeper hit for reusable mailers—it's thicker than standard nylon, wipes clean with a damp cloth, and the printed side hides scuffs better than any plain fabric. The key is that these materials don't just pretend to be reusable; they visibly age but still function.
One thing that separates survivors from wishful thinking is the closure. Snaps, heavy-duty zippers, and industrial Velcro outlast adhesive strips every time. And if a material can be repaired instead of retired—like re-welding a cracked plastic corner or patching a vinyl tear—it has a real shot at reaching 50 or 100 trips. That's the difference between a marketing claim and something that actually keeps boxes off the recycling line.
FAQ
Smart sensors that monitor fill levels and closure torque in real time, modular changeover systems for bottle shapes, and automated pressure adjustment on corkers and screw cappers are cutting downtime and product loss dramatically.
They shorten the gaps between bottle formats, let cleaning and filling happen in parallel, and predict mechanical wear before it causes a stoppage. The result is a higher overall equipment effectiveness score, not just a faster conveyor.
Vacuum filling combined with inert gas blanketing, inline dissolved oxygen sensors, and redesigned fill valves with smoother flow paths have been the most dependable ways to keep dissolved oxygen near zero without slowing the line.
Yes, many equipment builders now offer retrofit kits and compact monoblock units for rinsing, filling, and capping. Shared mobile bottling services also bring advanced packaging tech to small producers on a pay-per-bottle basis.
Analytics tracks fill volume drift, cap torque variance, and label alignment across thousands of bottles, then automatically nudges machine parameters. It catches slow shifts before they become rejected lots, cutting rework and material waste.
Lightweight glass, recycled PET bottles, low-flow rinsing nozzles, and energy-recovering motors are being built into high-speed lines. Optimized case and pallet patterns also reduce transport emissions while keeping throughput high.
Dedicated filling heads for carbonated and low-acid wine products now prevent foaming and oxygen ingress, while quick-swap tooling lets the same line handle cans, pouches, and traditional glass without a full teardown.
Collaborative robots for case packing and palletizing, vision systems that grade label and capsule quality in real time, and closed-loop controls that adjust the entire line based on upstream variations are all moving from pilot projects to standard installations.
Conclusion
At the heart of modern wine packaging facilities, a quiet revolution is underway—one that treats every bottle as a precision instrument rather than a mere container. Filling lines now trim waste down to the last milliliter, using flow meters and automated shutoff valves that respond in real time to each bottle's neck shape. The same machinery swaps between Burgundy and Bordeaux formats without stopping the belt, letting a single line handle half a dozen SKUs in a shift. Robotic arms with soft-touch grippers cradle each bottle through labeling and case packing, reducing scuffs that once plagued high-speed runs.
Cold-chain demands have pushed labeling materials forward: adhesives and face stocks now shrug off condensation, so bottles pulled from a 4°C cellar still look sharp on the shelf. Inline vision systems inspect fill height, cap torque, and label placement at 600 bottles per minute, flagging defects before they reach a pallet. Meanwhile, the shift toward reusable shipping materials has moved beyond token gestures—crates and dividers are now built from reinforced corrugate and folding sleeves that survive dozens of round trips. Together, these changes don't just speed up bottling; they reshape how a winery thinks about downtime, damage, and the liquid left in the hose.
Contact Us
Contact Person: Sunnie
Email: [email protected]
Tel/WhatsApp: +8615818596517
Website: https://www.imagine-craft.com/